AAA MOULD

AAA MOULD

Die Casting Design Guide

Design for manufacturing

Design rules that make die castings better and cheaper

Many die casting defects start on the drawing: porosity, cold shuts, sink marks, warpage and parts sticking in the die. The fixes are well known. Keep walls thin and even, add draft, radius the corners, replace thick sections with ribs, and decide early where the metal enters and where the air leaves.

We check every new part against these points and send DFM comments before die design starts. The values below are typical starting points; flow length, part size and alloy change them.

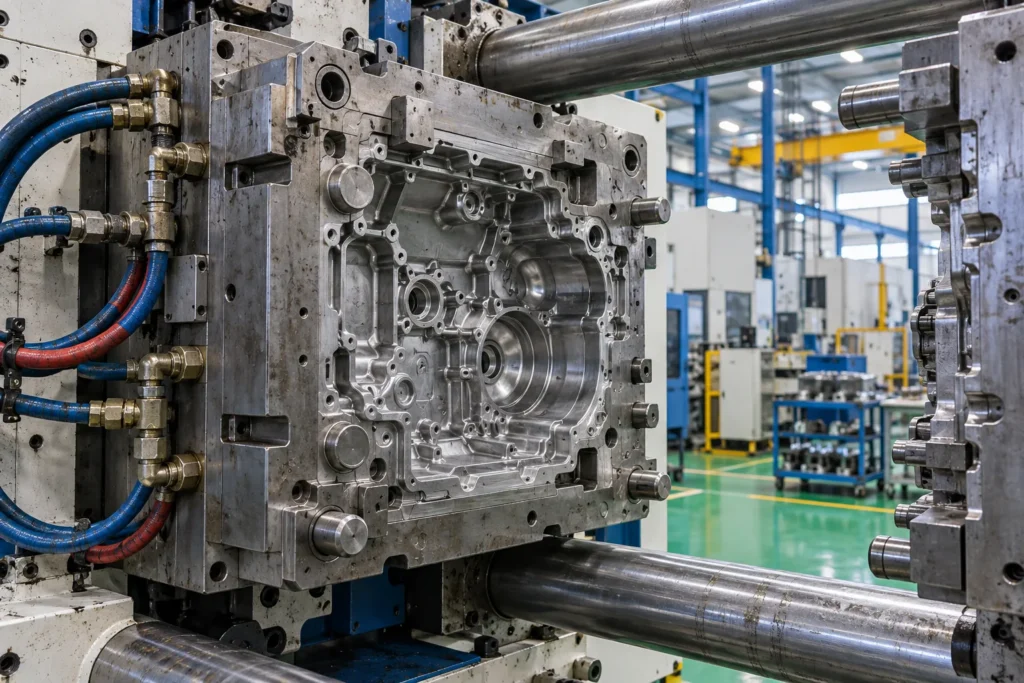
Open die casting die in the machine, cavity insert for an aluminum housing
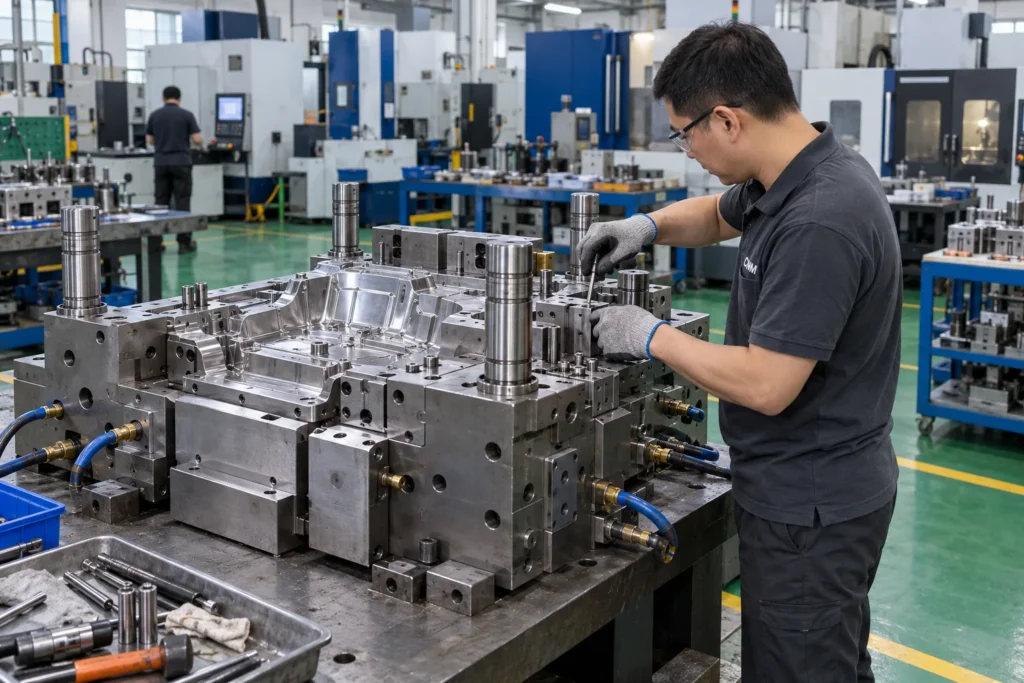
Toolmaker fitting a die casting die in the tool room

What our DFM review checks

Die casting design guidelines (typical)

Wall thicknessAluminum: typically about 1.5–4 mm; zinc: thinner possible; keep walls uniform
DraftAluminum: typically about 1–2°, more on inner walls and cores; zinc: about 0.5–1°
FilletsRadius all inside and outside corners; avoid sharp corners
RibsThinner than the adjoining wall, with draft and root radii
BossesCored out and tied to walls with ribs
HolesCored holes need draft; precise holes are machined
Machining stockTypically a few tenths of a millimeter up to about 1 mm
TolerancesGeneral tolerances to ISO 8062-3 or NADCA; tight features are machined

Design FAQ

Why are uniform walls important in die casting?

Metal in thick sections solidifies last and shrinks, which causes porosity and sink. Uniform walls fill and solidify evenly, so there are fewer defects and the cycle is shorter.

Can die castings have undercuts?

Yes, with slides or core pulls in the die, which add cost and maintenance. Redesigning a feature to avoid the undercut often lowers die cost.

Have a casting to quote? Tell us the part, the alloy and the annual volume.